


9mm EV Plywood: Core Options, Surface Quality and Flatness
A specification-led guide for buyers who need a firmer 9mm decorative plywood panel while controlling core construction, face quality, machining, documents and flatness.
Quick answer for plywood buyers
9mm engineered veneer plywood can be a reliable furniture and interior material when the complete panel is specified. Buyers should identify the face, back, core species, veneer schedule, glue system, finished thickness, moisture condition, surface finish and packing method. The product name alone does not establish those variables.
The practical purchasing question is not whether a species or face is “good.” It is whether the proposed construction suits the component and can repeatedly meet an agreed acceptance plan. 9mm improves handling rigidity within the thin-panel range; higher thickness does not remove the need for balanced construction; core choice still controls much of the weight, edge behaviour and hardware response. Samples should therefore be made with production-intent materials and tested after the planned machining and finishing steps.
For general thickness context, use Kosmex’s 6mm, 8mm and 9mm plywood guide. It explains why nominal thickness must be connected to span, support and finished dimensions rather than treated as a performance rating.
What 9mm EV plywood should mean in an RFQ
Commercial descriptions are often shorter than production specifications. A quotation may say only “9mm EV plywood,” while the factory still needs dozens of decisions. For this article, the product means 9mm engineered veneer plywood. The intended core is eucalyptus, poplar, pine or a documented combination construction. The visible surface is an engineered veneer face approved separately from the back and core. If any of these points can change without buyer approval, the product has not yet been fully defined.
Separate the face, back and core on the purchase document. The face controls appearance and part of the finishing response. The back contributes to balance and may have a different visual grade. The core forms most of the thickness and strongly affects weight, edge machining, screw response and stiffness. Adhesive controls bond performance under the named test and service condition. None of these variables should be inferred from the marketing name.
The quotation should also state sheet size, finished thickness range, squareness, diagonal tolerance, sanding or calibration, permitted repairs, edge quality, label system and unit packing. If the component fits a groove, confirm the finished dimension after decorative veneer, coating and sanding. If the edge remains visible, approve a cross-section rather than relying on face photographs.
Construction controls more than the species name
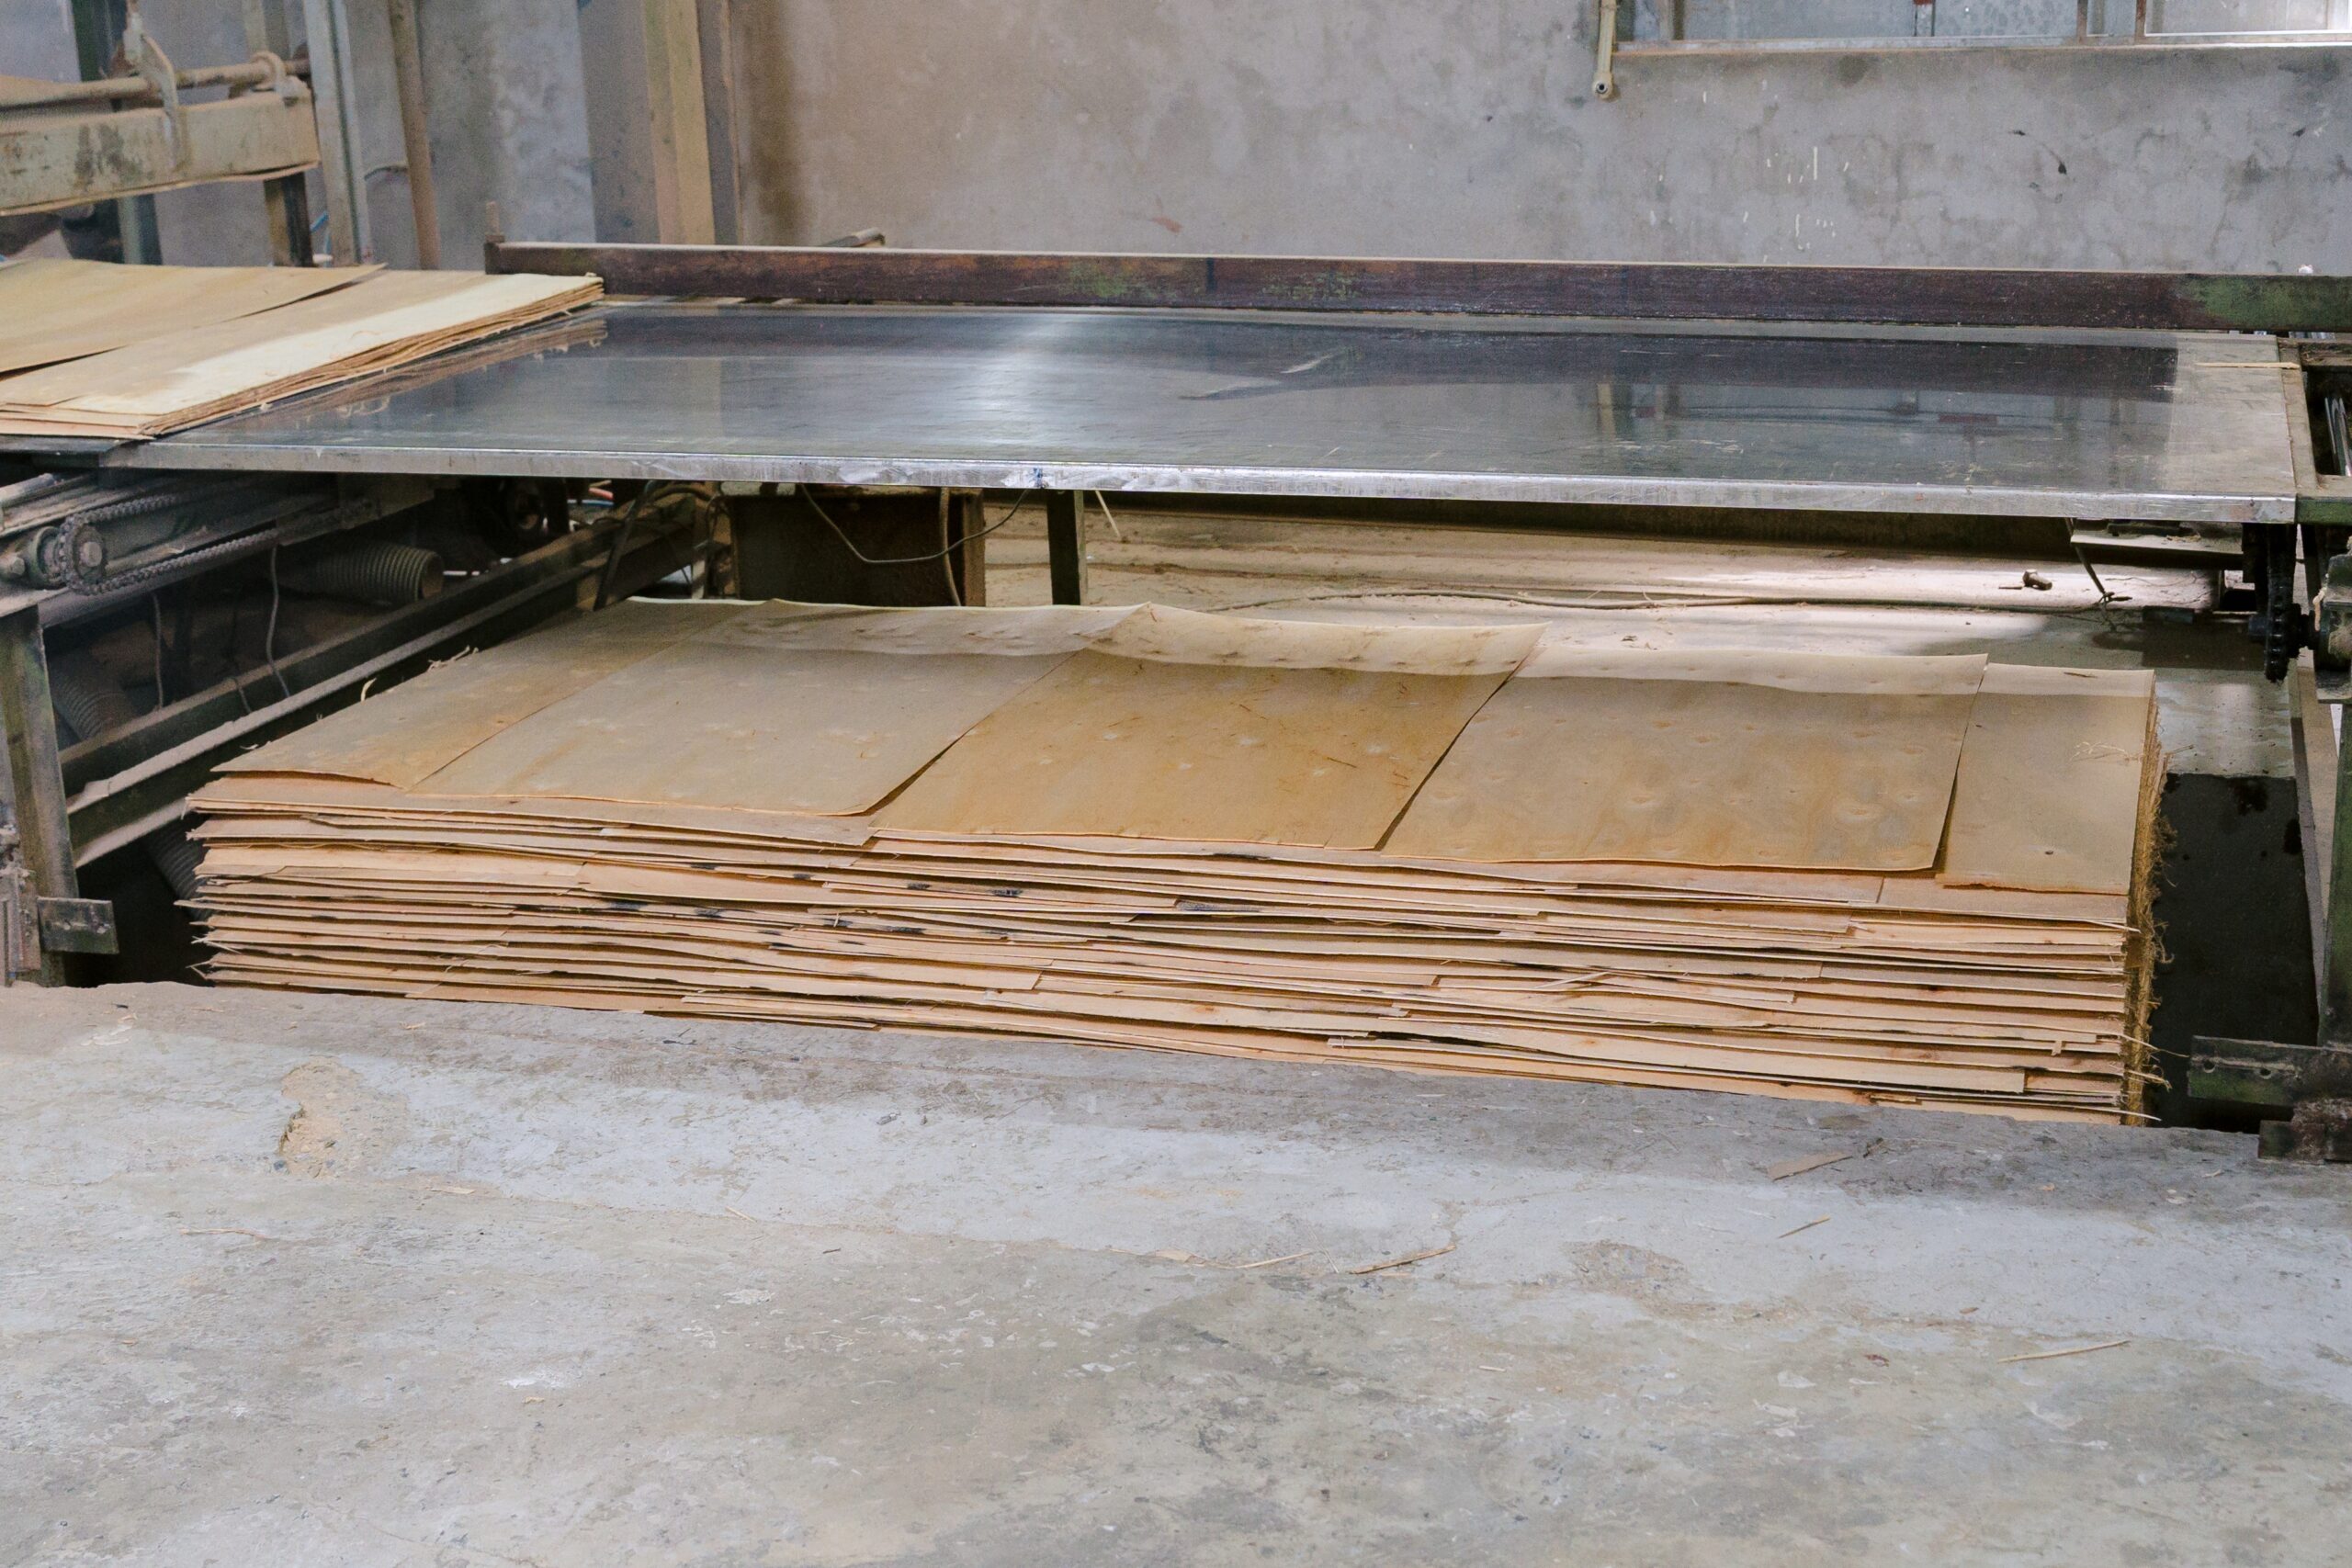
Plywood is a layered material. Veneers are arranged with alternating grain directions, bonded and pressed into a panel. A balanced design distributes movement and stress across the thickness. A panel can still curve when veneer moisture is unequal, the lay-up is asymmetric, glue spread varies, pressing is uneven or the finished faces exchange moisture at different rates.
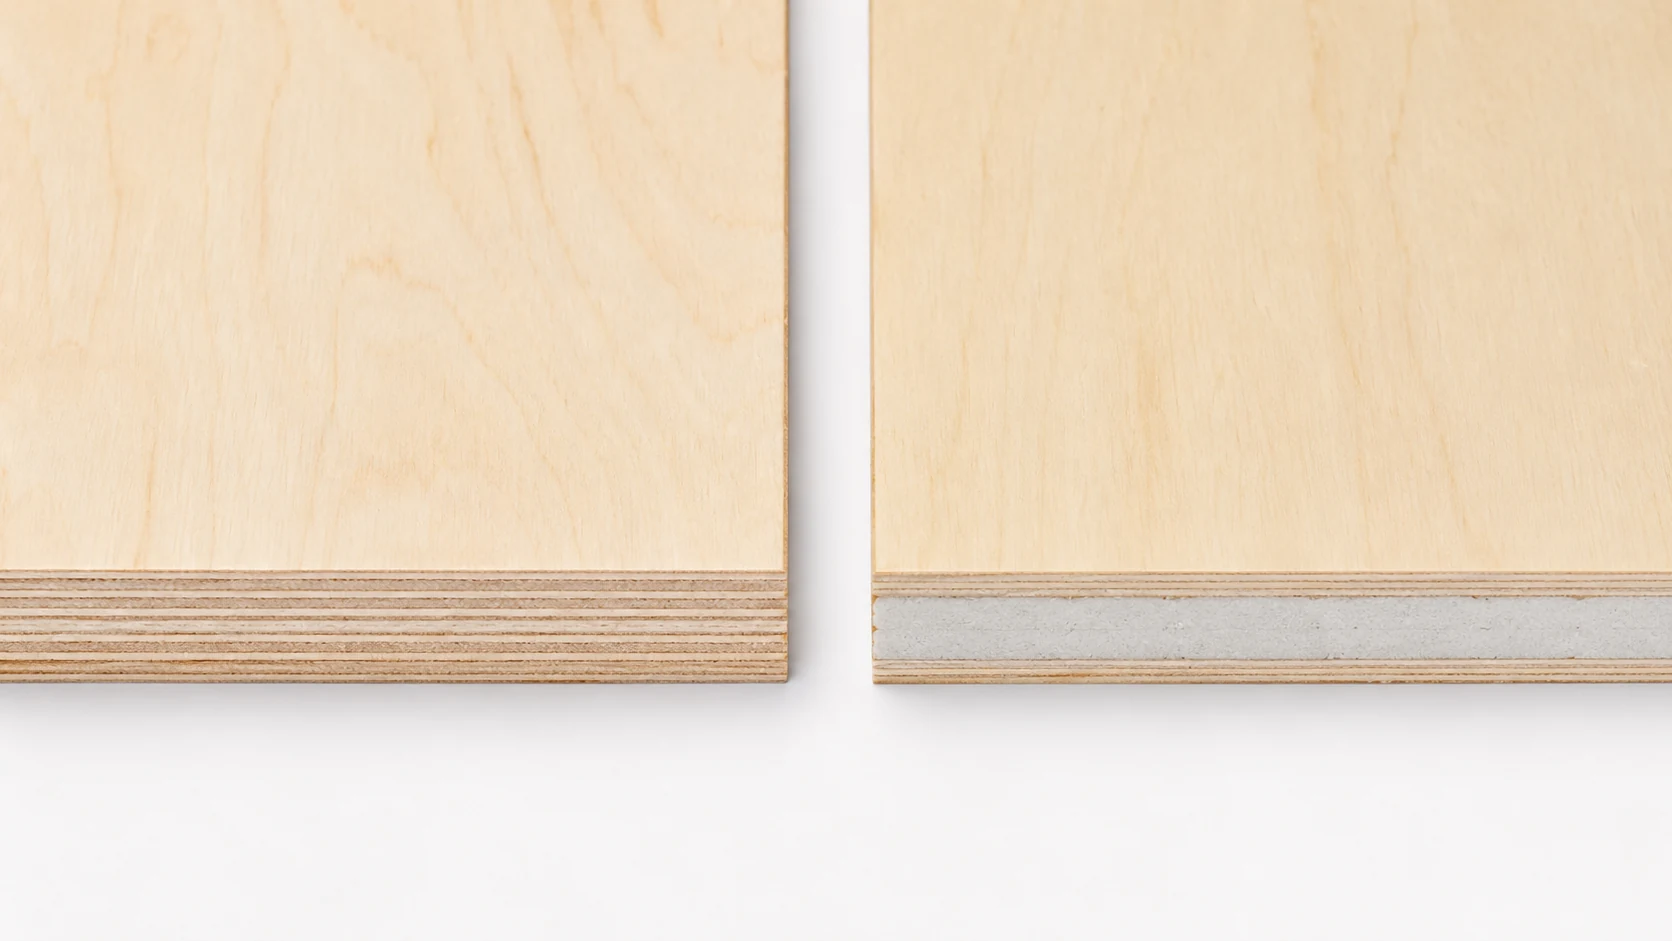
Ask the supplier for a construction schedule that names the species and approximate thickness of each ply or each functional layer. “Hardwood,” “combi” and “mixed core” are categories, not complete schedules. Buyers should know which species are permitted, where they appear and whether substitution requires written approval. A cross-cut sample reveals ply count, joints, gaps, overlaps and local compression that a face photo cannot show.
More plies are not automatically better. Thin, well-prepared veneers can help distribute stress and improve machining consistency, but poor joints or wet veneers remain defects. Likewise, a dense core may improve edge firmness while increasing shipping weight. Compare proposed constructions under the same thickness, face, back, moisture and test conditions.
How to select the right thickness and component
Thickness selection begins with the component, not a catalogue number. Provide finished part dimensions, unsupported span, orientation, fixing points, groove depth, hardware, expected load, finish and indoor climate. A thin sheet that is fully captured in a frame behaves differently from the same sheet used as a free-standing panel.
- Decorative furniture parts and cabinet elements. The final construction must be approved against component size, support, finish and service conditions.
- Supported partitions and door components. The final construction must be approved against component size, support, finish and service conditions.
- CNC-routed panels with visible faces. The final construction must be approved against component size, support, finish and service conditions.
- Retail, hospitality and repeated fit-out programmes. The final construction must be approved against component size, support, finish and service conditions.
Before production, cut and assemble representative parts. The trial should include the actual core, face, back, glue, coating, edge band and hardware. Observe breakout at drilled holes, edge crushing, groove fit, screw stripping, telegraphing and curvature after conditioning. Where a part carries load, run a component test with the intended support instead of relying on a broad species comparison.
Designers should also distinguish unwanted permanent warp from normal elastic deflection. Any thin panel can bend under its own weight or under load. Bow, cup and twist are geometry conditions measured without forcing the panel flat. Deflection is movement under a defined load and span. Combining these issues into the phrase “no bending” makes supplier evaluation impossible.
Flatness is a controlled result, not an absolute claim
The most common risks for this product include approving only the decorative face, leaving the back construction open, treating nominal thickness as finished thickness, assuming a thicker panel cannot warp, using test reports from a different construction. Each risk has a control. Veneers can be dried, sorted and matched. The lay-up can be balanced. Glue spread and press parameters can be monitored. Panels can be conditioned before sanding and grading. Finished bundles can be stacked on aligned bearers, protected from water and loaded without over-tight straps.
A supplier should not promise that wood panels will never move in every climate. A useful commitment is that identified samples, conditioned and supported as agreed, will remain within stated bow, cup and twist limits when measured by a defined method. This converts a slogan into an auditable purchase requirement.
Kosmex describes the production sequence in its plywood flatness-control guide. For shipment release, follow the flatness inspection procedure. These two documents should work together: process evidence reduces risk, while final inspection confirms the actual lot.
Bow, cup and twist are different
Bow is curvature mainly along the panel length. Cup is curvature across its width. Twist occurs when the corners do not lie in one plane. The inspection report should record each condition separately, including panel orientation, measurement location, support, maximum gap, direction and sample ID.
Do not measure on an unknown warehouse floor, press corners down by hand or photograph a gap without a scale. Use an agreed reference surface or support frame and suitable measuring equipment. For thin panels, allow the sheet to rest before recording the result and handle it without introducing a temporary bend.
Moisture, balancing and finishing
Wood veneer is hygroscopic. It gains and loses moisture as surrounding humidity changes. If one face changes faster than the other, the panel may curve even when it left the press flat. This is why veneer moisture matching, compatible face and back constructions, post-press conditioning and balanced finishing are central to thin-panel stability.
If the product will be painted, UV coated, laminated or veneered after shipment, test the complete system. Applying a low-permeability finish to one face while leaving the back open can create unequal moisture exchange. The reverse face does not always need the same appearance, but it should be technically compatible. Record coating weight, cure conditions and the time between finishing and inspection.
A moisture meter reading is useful only when the instrument and wood setting are appropriate. Measure a grid across several panels and both faces where the method allows. The goal is to identify gradients between faces, edges, centres and bundles. Moisture data helps explain movement, but it does not replace direct flatness measurement.
Machining and assembly trials
Furniture factories should test the operations that matter to production: panel sawing, CNC routing, drilling, grooving, edge banding, sanding, coating and fastening. Record tool, feed, speed and sample identity for critical trials. A good face does not prove that the core will machine cleanly or that edge screws will survive repeated assembly.
For decorative veneer, control sanding allowance so operators do not cut through the face. For visible edges, define gap and overlap limits and approve the appearance after cutting. For concealed edges, test the selected edge-band adhesive and press temperature. Hardware trials should use the exact screw, pilot hole, insertion torque and edge distance planned for the component.
Component yield belongs in the commercial comparison. A cheaper panel can cost more if it creates chipped edges, rejected colours, unstable parts or excessive tool wear. Ask the supplier to support a trial that measures usable pieces per sheet, machining time, rework and damage rather than comparing price per sheet alone.
Pre-shipment inspection plan
Define the inspection before production. State the lot, sampling plan, conditioning time, environment, support, instruments, measurement locations and acceptance limits. Samples should come from different bundles and positions, not only the easiest top sheet. Every photo should show a sample ID and enough context to repeat the check.
| Inspection area | What to record | Why it matters |
|---|---|---|
| Identity | PO, product code, lot, bundle and panel number | Connects results to released stock |
| Appearance | Face, back, colour range, repairs, sanding and edge damage | Confirms the approved visual standard |
| Dimensions | Thickness grid, length, width, diagonals and squareness | Protects machining and assembly fit |
| Construction | Ply count, named core, gaps, overlaps and open glue lines | Checks that production matches approval |
| Flatness | Bow, cup, twist, method, support and maximum gap | Creates a repeatable acceptance decision |
| Moisture | Instrument, setting, locations and range | Provides stability and diagnostic context |
| Packing | Bearer alignment, wrap, corners, straps, labels and loading photos | Preserves accepted quality during logistics |
If a sample fails, quarantine affected stock and record disposition. Do not simply replace the photographed sheet and release the bundle. Review production records and expand sampling as agreed. The corrective action should address cause, affected quantity, re-inspection and prevention.
Documents buyers should request
The document pack should match the offered construction and destination. Request a signed technical specification, approved master or reference sample, production and inspection records, packing specification and relevant test reports. A certificate title alone does not prove that the tested panel is identical to the order.
For each test report, check the laboratory, method, sample description, dimensions, conditioning, date and result. Bond performance, formaldehyde emission and mechanical properties use different methods and units. Do not transfer a result from another core, thickness or glue system without technical justification. Kosmex’s supplier document checklist gives procurement teams a practical evidence structure.
Where certification or chain-of-custody is required, state the exact scheme and claim in the RFQ. Confirm the legal entity, scope, validity and product connection. Keep commercial invoices, packing lists and bundle labels aligned with the controlled product name.
RFQ checklist for 9mm EV plywood
- Application: finished component, dimensions, support, span, load, hardware and service environment.
- Panel identity: 9mm engineered veneer plywood, face, back, core species and permitted substitutions.
- Dimensions: length, width, nominal and finished thickness, tolerance, squareness and diagonal limit.
- Surface: grade, pattern, colour range, sanding, repairs, coating and master-sample process.
- Bond and emissions: required method, class or limit and destination documentation.
- Flatness: conditioning, support, bow, cup and twist method, sampling and acceptance limits.
- Machining: saw, CNC, drilling, groove, edge band, finish and hardware trials.
- Packing: aligned bearers, protective sheet, wrap, strap position, labels and loading evidence.
- Change control: written approval before changes to face, core, glue, thickness or finish.
Common buying mistakes
- 1. Approving only the decorative face. Convert this risk into a named control, evidence field and acceptance decision before production.
- 2. Leaving the back construction open. Convert this risk into a named control, evidence field and acceptance decision before production.
- 3. Treating nominal thickness as finished thickness. Convert this risk into a named control, evidence field and acceptance decision before production.
- 4. Assuming a thicker panel cannot warp. Convert this risk into a named control, evidence field and acceptance decision before production.
- 5. Using test reports from a different construction. Convert this risk into a named control, evidence field and acceptance decision before production.
Another mistake is asking several suppliers for the same short product name and assuming their quotations describe equivalent panels. Align the construction and inspection fields first. Only then compare price, minimum order, lead time, packing, container utilisation and payment terms.
Finally, preserve the approved condition after inspection. Store bundles horizontally on level, aligned supports; protect them from rain and condensation; avoid local strap pressure; and acclimatise panels before machining when warehouse and production climates differ. The Kosmex storage and shipping guide connects factory quality with delivery condition.
How this article connects to the Kosmex content cluster
This guide is designed to support, not duplicate, the wider Kosmex knowledge base. Buyers can move from general selection to product-specific construction, then to factory control and pre-shipment evidence. Recommended next reading includes EV plywood complete guide, plywood flatness inspection, EV plywood versus natural veneer. Related application and supplier guidance includes documents to request from a supplier, common defects and prevention.
Internal links should remain descriptive. Avoid repeating an exact commercial keyword in every paragraph. When this page and its cluster pages are published together, add reciprocal links from the parent guide, relevant comparisons and QC pages so search engines and readers can understand the hierarchy.
Frequently asked questions
Can Kosmex supply panels that do not bend or warp?
Kosmex can engineer and manufacture panels to meet an agreed flatness specification, but no responsible supplier should promise zero movement in every climate, span and handling condition. Define the product, conditioning, support, measurement method, sample plan and limits for bow, cup and twist.
What is the most important sample to approve?
Approve a full production-intent panel whenever risk justifies it. A small swatch can confirm colour or face texture, but it cannot prove full-sheet pattern, core construction, machining yield, flatness or packing performance.
Does a thicker panel automatically stay flatter?
No. Greater thickness can improve handling stiffness, but permanent curvature can still result from moisture imbalance, asymmetric construction, finishing or poor support. Compare panels made and conditioned under equivalent conditions.
Which core is best?
There is no universal answer. Eucalyptus, Poplar, Pine and combination cores differ in density, machining, edge response, availability and cost. Select the core for the actual component and verify it with representative tests.
What should appear in the inspection report?
Include product and sample identity, environment, conditioning time, support, instrument and calibration status, measurement locations, results, photos with readable scale, acceptance limits and an authorised disposition.
Request a 9mm sample, core cross-section and test data
Send Kosmex the target thickness, sheet size, component drawing, face and back requirement, core preference, bond, finish, destination and flatness method. The team can review the specification and prepare a matching sample, quotation and inspection plan.
Bình luận